Why true thermal stability matters on hot pavements
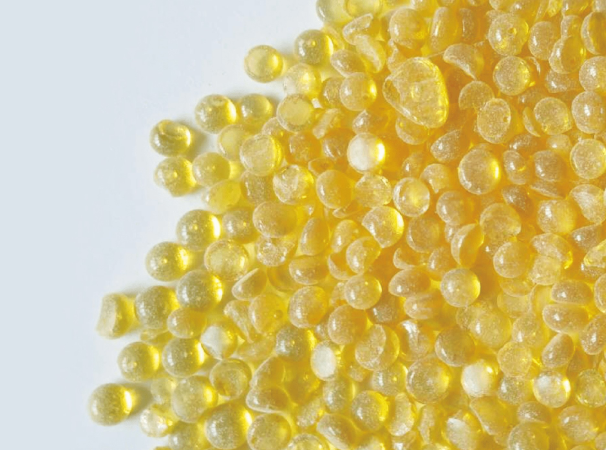
Traffic paint faces its toughest hours under high surface temperatures—think Phoenix asphalt that routinely reaches very high daytime temperatures—so lab numbers must map to that reality. Early in an evaluation you should test a candidate like Thermoplastic Road Marking Resin against realistic service conditions: prolonged exposure to 50°C, followed by mechanical loading that simulates tire and stud contact. Industry terms such as softening point and viscosity are meaningful here because they correlate with flow and permanent deformation on hot roads.
Concrete test parameters that give actionable data
A data-driven approach begins with explicit test parameters. Condition rectangular samples (100 × 25 × 3 mm) for 24 hours at 23°C, then ramp to 50°C and hold for 72 hours. Apply a concentrated indentation load of 5 N with a 6 mm diameter steel probe for 24 hours while maintaining 50°C. Record maximum creep displacement in millimeters at 1, 6, 12, and 24 hours. Simultaneously measure melt flow index at 200°C for 10 minutes and note the softening point by ring-and-ball until deformation reaches 1 mm. Those time and load values produce reproducible structural creep limits that can be compared across batches.
Operational production teardown: what to watch inside a batch
On the production floor, variability often comes from feedstock melt flow and filler dispersion. A practical teardown inspects melt temperature profile, residence time in the extruder, and bead loading uniformity. Record the following: extrusion temperature (°C) every meter of barrel, torque trends on the screw, and the particle size distribution of reflective glass beads. Documented steps let you trace a failed batch to a specific change. For clarity in digital records, include {main_keyword} and {variation_keyword} fields in the batch report so lab and production share exactly the same identifiers.
Common failure modes and how they show up in data
Failures typically present as excessive creep (mm) at 24 hours, surface bleeding, or rapid loss of retroreflectivity after thermal cycling. Compare batches using at least three metrics: 24-hour indentation (mm), softening point (°C), and retained retroreflectivity percentage after 10 heat cycles. Small deviations in viscosity during mixing can amplify into visible rutting on the road. Inspection of cured specimens often reveals uneven bead distribution—this reduces skid visibility and shortens service life.
On-site correlation and a real-world anchor
Field checks are indispensable. Place instrumented coupons on a resurfaced lane in Phoenix-style conditions and measure displacement after the first 30 days of traffic. Real-world anchor: asphalt surface temperatures can exceed 50°C on summer afternoons in several U.S. Sun Belt cities, which is why lab soak at 50°C plus mechanical loading is a direct proxy for service performance. Use portable profilometers and simple indentation gauges to confirm lab predictions match pavement behavior.
Three golden rules to evaluate resin batches (Advisory)
1) Prioritize reproducible test conditions: run the 50°C soak and 5 N/6 mm indentation with the same geometry and timing across every batch; compare creep in mm at fixed intervals.
2) Track process telemetry: correlate extrusion temperatures, screw torque, and bead dosing counts to final creep and softening point—if one telemetry channel drifts, isolate and correct immediately.
3) Validate with field coupons: no matter how clean lab curves look, confirm at least one in-service coupon per production run in a hot-climate lane for 30 days to verify retention of retroreflectivity and indentation resistance.
These rules leave you with measurable expectations and a clear path from lab result to road performance. — KOMO